Australian Market Production Roster & Cut Profiles
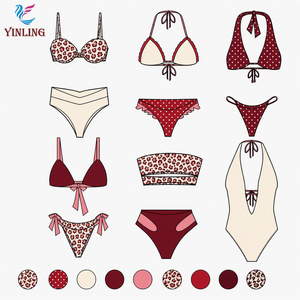
Explore eight core performance silhouettes, training cuts, and promotional capsule styles engineered with reinforced dual-needle lockstitch flat seams, chlorine-proof polybutylene lining, and bespoke branding.
Technical Whitepaper: Engineering High-Performance Team Swimwear for the Australian Biosphere
Australia boasts one of the most rigorous, high-exposure aquatic environments in the world. From the hyper-saline, turbulent shorebreaks negotiated by Surf Life Saving Australia (SLSA) competitors to the heavy commercial hyper-chlorinated facilities of state aquatic centers in Sydney, Melbourne, and Brisbane, standard off-the-shelf recreational swimwear degrades prematurely. Fiber embrittlement, micro-fissuring of polyurethane elastane, pigment bleeding, and UV-induced structural sag present severe financial and logistical liabilities for club procurement boards, school sports associations, and private label activewear brands.
As a seasoned OEM/ODM swimwear manufacturing powerhouse operating an elite sampling and scalable bulk production infrastructure since 1993, we offer Australian team directors, collegiate athletic leagues, and commercial brands a direct-factory engineering partnership. Our manufacturing core unites state-of-the-art Italian circular knitting substrates (such as Carvico Vita and Jersey Lomellina), post-consumer recycled ECONYL® and REPREVE® polyesters, alongside specialized Polybutylene Terephthalate (PBT) chlorine-blocking yarns. By controlling pattern drafting in 2D AutoCAD, implementing digital sublimation calibration with zero color drift across multiple print batches, and backing every seam with stretch flatlock thread, we ensure Australian aquatic outfits receive institutional-grade longevity.
Semantic Search & Supply Chain Integrity Notice
This technical overview details factory-floor grading, chemical resistance protocols, and logistical operations for B2B procurement officers seeking low-MOQ, high-mix OEM/ODM custom team swimwear exporter channels to Australian ports with guaranteed lead times and certified ethical compliance.
Hydrodynamic Resistance vs. Photolytic Stability: The Dual Challenge of Oceanic & Pool Use
When engineering team swimwear for Australian competitive squads, fabric selection cannot follow generic activewear conventions. Pool training environments use sodium hypochlorite or salt-cell chlorine generation creating hypochlorous acid (HOCl). This compound attacks standard elastane, stripping its tensile elastic recovery within 30 to 45 hours of cumulative exposure. To counter this, our technical team blends PBT (Polybutylene Terephthalate) fibers with modified polyester, creating an isometric lattice that retains 95% of its initial modulus over 240+ hours in chlorine concentrations up to 4.0 ppm.
Simultaneously, open-water training along the Gold Coast, Perth beaches, and Victoria’s Bellarine Peninsula demands compliance with Australia's mandatory AS/NZS 4399:2020 sun protection clothing regulations. We utilize high-density warp-knit fabric construction (220 to 260 GSM) that blocks 98%+ of harmful ultraviolet UVA and UVB spectrum radiation without relying purely on topical chemical coatings that wash out after consecutive dips. Every batch exported into Australia is tested for ultraviolet transmittance, dry and wet tensile elongation, and colorfastness against sea salt, pool water, and perspiration.
Localized Australian Applications & Team Form Factors
Bespoke athletic patterning tailored to Australian physique demographics, sporting disciplines, and club governance frameworks.
Surf Life Saving Clubs (SLSC) & Nippers
Engineered for explosive shore-break resistance, sand abrasion friction, and sun safety. We manufacture high-visibility skull caps, compression one-piece suits with cross-back tensioning, and high-mobility two-piece costumes featuring dual-layer bar-tacked waistbands that will not shift during board paddle or surf boat rowing events.
GPS & APS School Aquatic Programs
Private collegiate associations across New South Wales, Victoria, and Queensland require strict heraldic PMS color matching and uniform discipline. We deliver custom dyed-to-match team one-pieces, jammer trunks, and silicone cap kits featuring institutional cresting, reinforced gusset linings, and athletic modesty cuts.
Triathlon Squads & Ocean Swimming
High-stroke repetition demands zero chafing under low-profile arm and neck openings. Our seamless edge bonding, bonded silicone micro-bead grippers, and hydro-glide hydrophobic coatings ensure triathletes maintain low drag in the water and immediate rapid-dry transition times when exiting transition zones.
Water Polo Leagues & High-Impact Squads
Water polo demands high shear resistance and non-grab form contours. We produce industrial zip-back one-pieces and heavy-duty front-tie briefs constructed with dual-ply PBT laminations and reinforced flatlock overstitching that prevents seam splitting under aggressive competitive handling.
Corporate & Charity Open-Water Events
From the Rottnest Channel Swim in WA to the Lorne Pier to Pub in VIC, we produce custom turnkey race kits including matching team rash vests, transition towels, sun-protective bucket hats, and bespoke printed briefs that elevate sponsor visibility.
Commercial Boutique Private Labels
For independent Aussie designers seeking to launch sustainable resort and training hybrids, we offer full private-label support: custom heat-sealed silicone care labels, FSC-certified recycled card hang tags, and biodegradable polybags designed for immediate local retail shelf-placement.
Australian Market Dynamics: Macro Trends Influencing Swimwear Sourcing
The Australian swimwear procurement sector is undergoing an unprecedented structural transition driven by ESG (Environmental, Social, and Governance) compliance mandates, regional circular economy targets, and supply chain de-risking. Sourcing directors across municipal clubs, sporting federations, and fashion retail chains are no longer willing to tolerate opacity in factory worker conditions or toxic non-traceable chemical dyeing processes.
1. The Circular Fabric Mandate (ECONYL® & REPREVE® Standard)
Australian consumers and school councils actively prefer athletic garments that tell an environmental restoration story. The utilization of regenerated ocean nylon derived from ghost fishing nets and post-industrial carpet fibers (such as Carvico Vita featuring ECONYL®) has evolved from a premium marketing luxury into a baseline tender requirement. Our factory holds Global Recycled Standard (GRS) and OEKO-TEX® Standard 100 certifications, validating that zero hazardous chemical effluent enters waterways during our digital printing and immersion dyeing operations.
2. Hyper-Localized Short-Run Collections & De-Stocking Strategies
The historical procurement approach of ordering 5,000 units per style from legacy mass-production vendors is obsolete for modern Australian sports clubs. Cash flow optimization requires low Minimum Order Quantities (MOQs) broken across a diversified collection of styles, cuts, and body types. Our production architecture—allowing collection MOQs starting at 300 to 400 pieces with per-style allocations as low as 30 to 40 pieces—enables club merchandisers to sample, test, and restock hot sizes within a 3 to 5-week manufacturing window.
| Performance Property | Standard Spandex / Nylon | Carvico Vita (ECONYL®) | PBT Industrial Tech Blend |
|---|---|---|---|
| Chlorine Degradation Threshold | 40–60 Pool Hours | 180–220 Pool Hours | 300+ Continuous Hours |
| UV Protection Factor (AS/NZS 4399) | UPF 20–30 (Degrades over time) | UPF 50+ (Certified Permanent) | UPF 50+ (Certified Permanent) |
| Tensile Recovery & Modulus | Rapid sag after 30 days | Superior shape retention | Mechanical snap-back memory |
| Environmental Certification | Petrochemical Virgin Synthetics | GRS Certified / Recycled | Available in Recycled Blends |
| Print Resolution Fidelity | Standard 300 DPI Sublimation | Ultra-deep 720 DPI Digital Ink | Vibrant, Fade-Proof Calibration |
Factory-Direct Engineering: The Proven OEM/ODM Manufacturing Advantage
Operating continuously since 1993 with a dedicated studio of over 65 in-house specialists, our production facility in Kerobokan bridges the gap between high-fashion couture finishing and rugged athletic teamwear manufacturing. When you partner with us for the Australian market, you eliminate intermediary trading brokers, excessive agency markups, and communication errors.
2D AutoCAD Pattern Drafting
Every team swimwear profile is drafted within digital 2D AutoCAD suites, enabling micrometric adjustments to torso lengths, leg opening depths, and bust-support arch lines. This allows us to rapidly translate physical design sketches or 2D technical specs into production-ready marker grading across youth, women’s, and men’s athletic sizes.
Italian MS Digital Direct Printing
We deploy industrial-grade Italian MS digital sublimation machines paired with environmentally friendly aqueous inks. Artwork files reproduce with edge-to-edge Pantone precision, razor-sharp logo resolution, and deep black saturation without the stiff surface film typical of low-tier transfer prints.
Duty-Efficient Import Facilities
Benefiting from official tax-free raw material import licenses, we stock over 200+ premium Italian and American fabric shades on our warehouse floor. By bypassing local import tariffs on virgin fabrics, we pass on up to a 35% raw material cost saving directly to your unit economics.
Frequently Asked Questions for Australian B2B Sourcing
Transparent operational answers addressing logistics, tariff structures, production lead times, and sampling guarantees.
What are the collection MOQs for Australian club or team orders?
Our minimum order quantities are established per collection rather than forcing massive volumes per single SKU. For fully custom OEM designs (your exact tech pack, custom cut, and specific branding), our collection MOQ is 400 pieces, requiring only 40 pieces per style distributed across a minimum of 4 pieces per size/color. For our curated Ready Design white-label team styles, the collection MOQ drops to 300 pieces (30 per style), allowing flexible sizing curves across your squad roster.
What is the sample turn-around time before bulk sign-off?
Using our extensive in-house stock of Italian Carvico Vita, Sumatra, Pantelleria, or Eco Lustra fabrics, custom physical counter-samples take between 1 to 3 weeks to engineer, stitch, and dispatch. Ready Design samples are dispatched in 1 to 2 weeks. Custom sample development fees are 100% credited against your final bulk production invoice deposit once the collection is green-lit.
How do shipping and Australian import customs operate?
We ship air express via DHL Worldwide Express directly to commercial addresses, clubrooms, or fulfillment centers across Sydney, Melbourne, Brisbane, Perth, and Adelaide in 3 to 5 business days. Bulk freight averages approximately USD $1.30 to $2.00 per garment. For Australian shipments entering under the A$1,000 threshold, customs clearance is streamlined; for orders exceeding A$1,000, our freight forwarding documentation includes clear HS code declarations and commercial invoices to simplify GST and duty clearance.
How do we ensure brand exclusivity and pattern security?
We are strictly a business-to-business (B2B) original equipment manufacturer and exporter. We do not operate competing consumer-facing retail brands or sell off our clients' excess inventory. Any proprietary CAD pattern files, custom digital print artwork, and club heraldic branding assets submitted to our studio are protected under mutual Non-Disclosure Agreements (NDAs) and stored on secure enterprise servers.
Are your fabrics tested for UPF 50+ compliance in Australia?
Yes. All our recycled nylon and polyester swim textiles comply with the stringent AS/NZS 4399:2020 standard, delivering UPF 50+ protection that shields athletes against 98% of harmful cellular UVA/UVB radiation. Full fabric certification documentation, OEKO-TEX® chemical clearance sheets, and GRS batch transaction certificates are available upon request during sample staging.
What happens if a production batch deviates from approved samples?
We back our manufacturing output with an ironclad quality assurance guarantee. Every production phase is overseen by your assigned product development coordinator. If an exported batch exhibits dimensional deviation outside standard AQL 2.5 textile tolerances or displays printing errors that diverge from the sign-off sample, we adjust the pattern in 2D AutoCAD and remake or credit the affected units immediately without friction.
Begin Your Team Swimwear Manufacturing Consultation
Connect with our technical product development coordinators today. Submit your CAD tech packs, mood boards, or club brand colors to receive a finalized quotation and fabric allocation plan within 48 to 72 hours.
Get Catalog